 CN


Welcome to call for consultation
Professional technical consultants are at your service 24 hours a day!
 0519-86153308
 czhddl@163.com
Contact Us

 Page views:Update time:
 Product Introduction
1. Working Principle
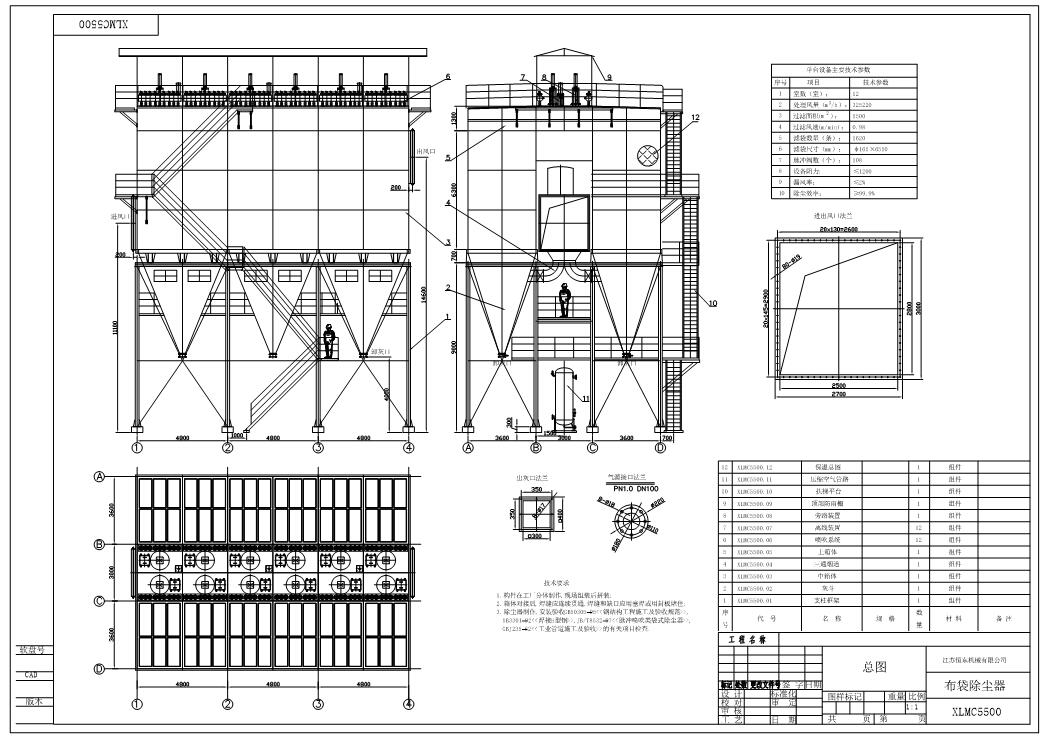
The XLMC off-line ash-cleaning low-pressure pulse baghouse filter adopts the outer filtration type for gas purification. Dust-laden gas enters each unit filter chamber through the guide pipe and passes through the flue gas guiding device installed in the hopper. As a sufficient and reasonable vertical clearance is reserved between the bag bottom and the upper opening of the air inlet in the design, the air flow is properly guided and naturally distributed to achieve uniform airflow distribution in the entire filter chamber. After separation by natural sedimentation, granular dust in the dust-laden gas falls directly into the hopper. Guided by the flow guiding system, the remaining dust enters the filtering area of the middle box along with the airflow and adheres to the outer surface of the filter bags. The purified gas after filtration penetrates the filter bags and is discharged through the upper box and exhaust duct.
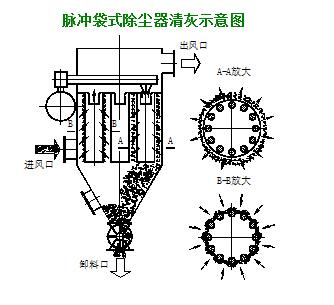
The filter bags are cleaned by jetting compressed air. The ash cleaning mechanism consists of a main jet pipe, branch jet pipes, electromagnetic pulse control valves and other components. A jet pipe is installed at the top of the outlet of each row of filter bags inside the filter chamber. Jet nozzles are arranged on the lower side of each jet pipe, directly facing the center of the filter bags. Each jet pipe is equipped with a pulse valve connected to a compressed air air tank. During ash cleaning, the solenoid valve opens the pulse valve, and compressed air is jetted toward the filter bag through the nozzle. Together with the surrounding entrained air, it shoots into the filter bag, causing the filter bag to shake fully and generating an outward reverse airflow, which removes dust adhering to the outer surface of the filter bag to achieve ash cleaning.
As the filtration process proceeds, when the dust accumulation on the surface of the filter bags reaches a certain level, the ash cleaning control device (differential pressure, timing or manual control) opens the electromagnetic pulse valves for jetting according to the set program. Compressed gas passes through each pulse valve in an extremely short time, and the nozzles on the jet pipes induce air several times the injection volume into the filter bags to form air waves. This causes rapid expansion and impact vibration of the filter bags from the bag opening to the bottom, producing a strong ash cleaning effect and shaking off the dust on the filter bags.
Pre-coating is performed before the dust collector is put into operation to protect the filter bags; the pre-coating device is activated for pipeline powder injection to protect the filter bags when the boiler operates with oil at low load and at the initial stage of "four-tube" rupture; the bypass protection system is started during boiler oil-firing startup, "four-tube" rupture and abnormal flue gas temperature.
Dust falling into the ash hopper is discharged from the outlet and then conveyed centrally by ash conveying facilities.
The dust collector is equipped with on-line and off-line dust cleaning functions as well as an off-line maintenance function.
The dust collector is fitted with a filter bag leak detection device to check the condition of filter bags, together with on-line monitoring devices for differential pressure, temperature, material level and other parameters.
The control of the dust collector (including dust cleaning control) adopts PLC control. The whole dust removal system realizes automatic unattended control, can feed back information to the plant master system and accept remote control from the plant master system.
All maintenance and overhaul work is carried out in the clean gas chamber of the dust collector and outside the equipment, with no need to enter the interior of the dust collector.
2. Technical Features
The development and commissioning of the XLMC high-efficiency low-pressure pulse bag dust collector incorporates the expertise of numerous industry specialists, with many of the company’s technical staff devoting tremendous efforts to it. Functions including low-pressure pulse, off-line dust cleaning, non-stop maintenance and protection technologies have been added to the dust collector in accordance with the flue gas characteristics of utility boilers and power plant operation requirements. These features have gradually demonstrated their advantages and gained increasing recognition and praise from design institutes and power plants. Its technical characteristics that distinguish it from pulse bag dust collectors used in other industries are as follows:
1) Low-pressure injection technology
Given the high concentration of flue dust generated by the combustion of utility boilers, the equipment resistance rises rapidly and the dust cleaning frequency increases accordingly. High-pressure injection will exert an adverse impact on the service life of filter bags. In addition, the dust cake attached to filter bags will be completely blown away, which not only prevents dust from falling into the ash hopper by its own gravity, but also tends to cause secondary re-adhesion of dust.
On-site monitoring with camera probes shows that the fly ash in flue gas is relatively dry under working temperature conditions. Combined with the easy-cleaning treatment applied to filter bags, dust cleaning at a relatively low pressure can achieve ideal cleaning performance and shorten the time for dust to settle into the ash hopper. It can avoid secondary re-adhesion and the reduction of filter bag service life caused by frequent dust cleaning.
2) Flow guiding technology
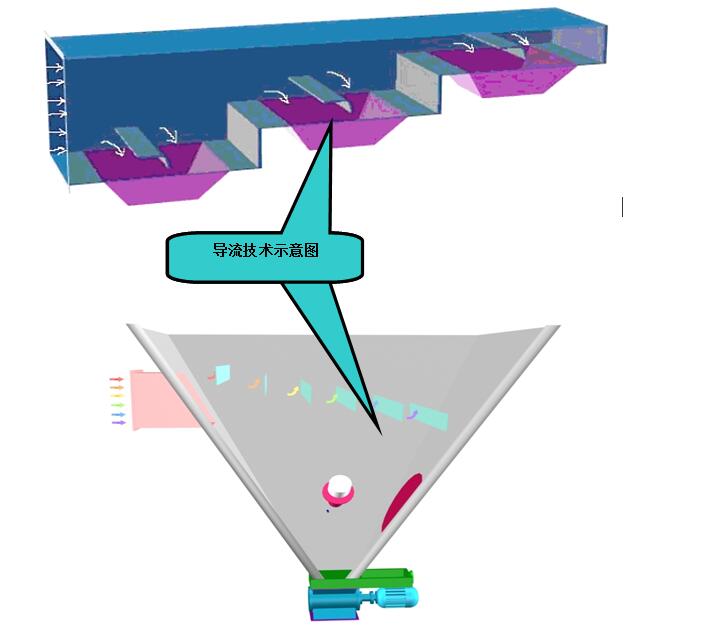
Solenoid pulse valves and filter bags are the core components of the XLMC high-efficiency low-pressure pulse bag dust collector, and flow guiding serves as the core technology. In line with our company’s design philosophy, a series of measures are adopted to achieve even distribution of flue gas to each filter bag. This ensures uniform load on filter bags to extend their service life while substantially reducing equipment resistance.
3) Offline Ash Cleaning / Non-stop Maintenance Technology
To ensure more thorough and effective ash cleaning, a pneumatic lift valve is installed at the air outlet of each unit bin. This allows the target bin requiring ash cleaning to be isolated independently. Ash cleaning will not be disturbed by the upward airflow, shortening the settling time of dust.
The pneumatic lift valve adopts a pneumatic thin-plate quick-opening structure. Its whole opening and closing process is linear motion, with auxiliary guide slide rails for accurate positioning. This avoids the high failure rate common to rotating structures under high-temperature conditions.
By closing the pneumatic lift valve and the manual air regulating valve at the ash hopper inlet, maintenance work such as filter bag replacement in the current bin can be carried out, while all other operations are performed outside the equipment, realizing non-stop maintenance.
4) Fixed Pipe Jet Ash Cleaning Technology
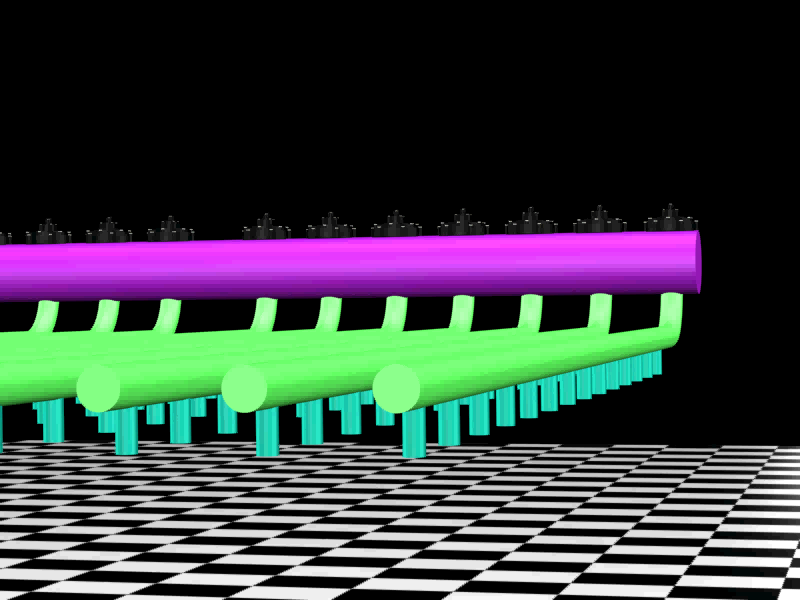
Fixed pipe jet ash cleaning technology is widely adopted in the dust removal industry today. It eliminates the drawbacks of rotary jet systems, including vulnerable bearings and difficult lubrication that lead to high failure rates. It also solves the problem of persistently high equipment resistance caused by incomplete reverse air ash cleaning.
Treated compressed air induces clean air from the upper box to jet instantly into the inner cylinder of the filter bag, generating pulse vibration. Dust adhered to the outer surface of the filter bag detaches from the bag and falls into the ash hopper under this sudden intense vibration.
5) Fixed Jet Pipe
6) Bypass Protection Technology
The dust collector is equipped with a built-in bypass, which is aesthetic and practical. The system automatically opens the bypass under the following conditions:
① When the temperature at the boiler tail outlet exceeds the allowable operating temperature of the selected bag filter material;
② When tube burst occurs in the water wall, superheater, reheater or economizer during boiler operation;
③ During boiler startup with full oil firing, mixed combustion of oil and coal, or oil-assisted combustion under low load;
④ When other conditions that affect the service life of filter bags occur.
While the bypass protection technology protects the filter bags, it cannot guarantee the flue gas emission concentration. The boiler shall be overhauled as soon as possible to restore the normal (automatic) operation of the dust collector.
7) High-temperature Resistant Filter Material Application Technology
Based on the flue gas conditions of power plants and the application of PPS filter material at the boiler tails in China’s power industry, PPS filter material is found to be an economical filter material suitable for dust removal at boiler tails in the power industry. Moreover, the service life of PPS filter material is further prolonged after anti-oxidation, acid-resistant and alkali-resistant treatment.
The filter bag can withstand an oxygen content of 8% in flue gas. When this value is exceeded, the dust collector operates with the bypass open.
When the flue gas temperature is lower than 100℃, the filter bags are prone to acid corrosion, and the dust collector operates with the bypass open.
8) Application of Detection and Monitoring Technology: In accordance with the operating characteristics of the dust collector, advanced on-line detection and monitoring devices are installed for flue gas temperature, dust collector operating pressure, material level, and fault detection of operating equipment.
9) The application of PLC programmable logic controller realizes automatic control of the dust collector as a major operating equipment of the power plant.
10) Equipment Resistance Control: Through a series of unique considerations in equipment design, the safety and reliability of the overall equipment resistance are guaranteed from both the equipment structure and filter material aspects.
The adoption of a series of advanced technologies ensures that the dust collectors manufactured by our company feature first-class technology and excellent cost-performance ratio.
Previous: Wet Electrostatic Precipitator
 Online Message
Welcome to call for consultation
Professional technical consultants are at your service 24 hours a day!
0519-86153308
czhddl@163.com
Contact Us
 Product Center
 Related Articles